Table of Contents
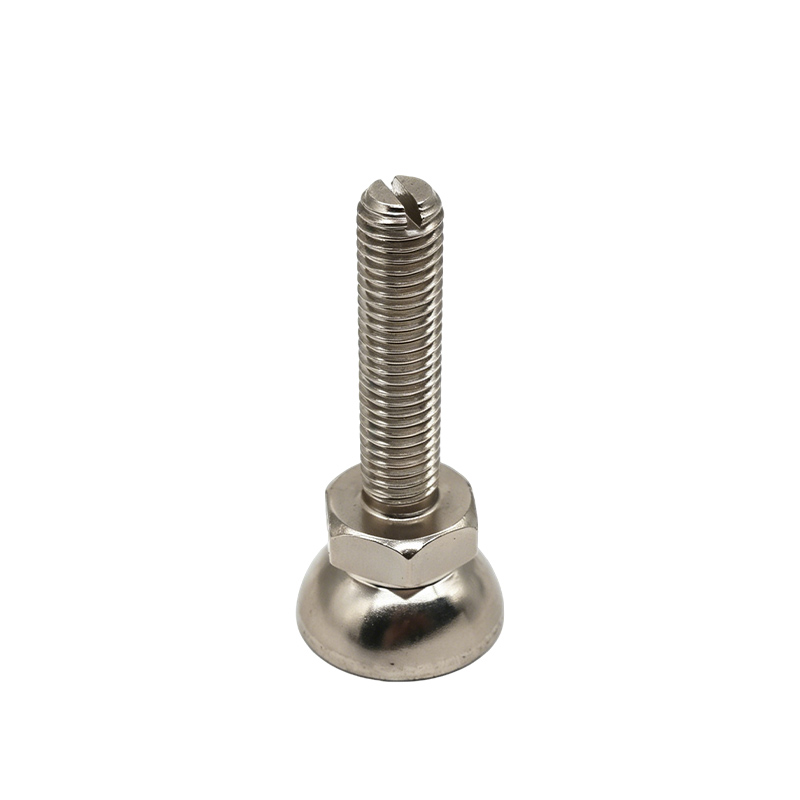
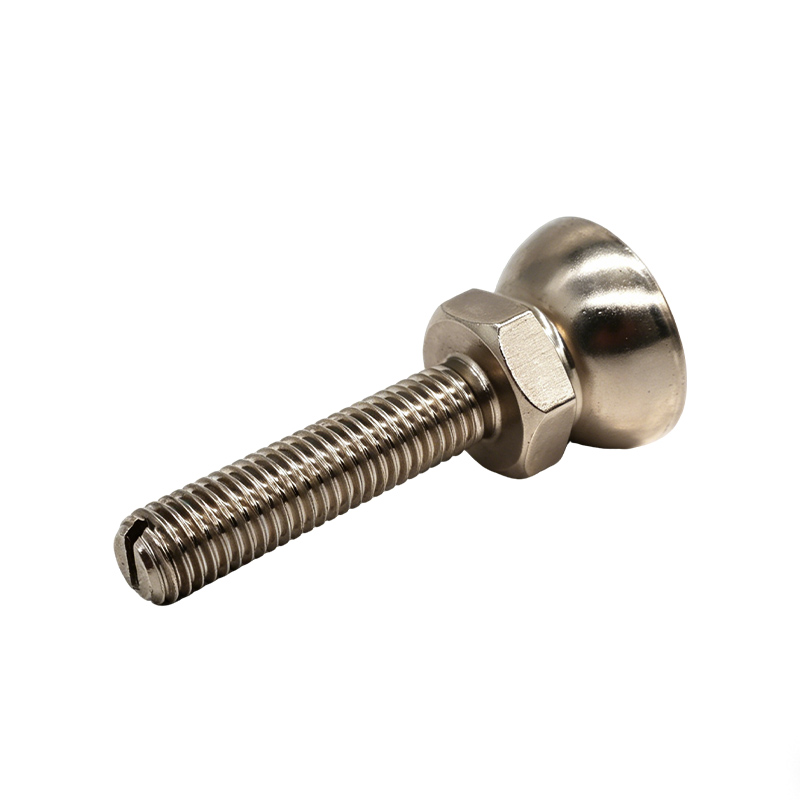
For buyers sourcing precision threaded rod, this review focuses on socket contact. The component example is the m12 ball head upper pressure rod. The first decision is which surfaces establish position and which surfaces need clearance. A dimension becomes useful only when its role in the assembly is clear.
Define the working interface for precision threaded rod
A ball head needs a defined contact envelope and a compatible socket. The ball radius alone does not establish freedom of movement or retention. Review the neck transition and the intended angular travel together so that one feature does not become the unintended motion stop. For precision threaded rod, start by identifying the mating socket and threaded connection. Mark the surfaces that locate, support or transmit force and keep them distinct from clearance surfaces. This gives the supplier a functional reason for each important dimension instead of asking for equal precision everywhere.
Connect the features to a datum
Review ball head, wrench flats and threaded shank as one geometry. The drawing should show how the features relate to a repeatable reference. If the reference exists only in the assembled product, provide enough mating information for the manufacturer to reproduce it during inspection. In the ball head rods example, the review therefore follows the ball head, wrench flats and threaded shank through the drawing and the assembled position.
Separate nominal size from usable contact
The practical question for precision threaded rod is where contact occurs after full seating. Lead-ins, corner radii and transitions can reduce usable engagement without changing the envelope dimension. Review a section view and define the intended contact zone before deciding which tolerances to tighten.
Compare the available design decisions
Keep the baseline drawing beside any proposed revision. A wider clearance may simplify assembly while changing movement or contact. A tighter size may increase inspection or finishing requirements. Evaluate the change against the function it affects and record the accepted trade-off.
| Review choice | Useful evidence | Decision limit |
|---|---|---|
| Drawing dimensions | Actual results tied to datums and final condition | Does not alone validate the complete assembly |
| Functional or profile gauge | Controlled master and documented check coverage | Only proves characteristics the gauge evaluates |
| Representative assembly trial | Identified mating parts and repeatable observations | System load and life tests remain application-specific |
Evaluate the manufacturing route
For this example, the site lists 40Cr. The material label does not establish what every version of precision threaded rod can achieve. Ask which features can be formed directly, which need another operation, and which dimensions will be verified after the final processing step. The listed material is a product-page reference for this example. Confirm the controlled specification for the actual order rather than importing the catalog's approximate grade equivalents.
Build a representative fit trial for precision threaded rod
Test precision threaded rod with a controlled mating component, identified by revision. Record entry, seating and the final operating position separately. If the trial fails, preserve the contact evidence and measurement setup so a drawing change addresses the actual interface rather than an assumed cause.
Set an approval boundary
Release the geometry with defined dimensions, references and accepted evidence. A successful hand fit is useful feedback but does not replace the specified component checks or system qualification. For precision threaded rod, preserve the approved sample alongside the drawing rather than letting either become an uncontrolled substitute.
Prepare the supplier discussion
Send the current drawing, mating envelope and the specific fit concern. For precision threaded rod, ask for a feature-by-feature feasibility response and a clear description of any proposed departure. The resulting quotation should identify the drawing revision and the condition in which the part will be supplied.
For further background, consult NIST guidance on measurement process characterization. This independent resource supports the review method; it does not certify the component or replace its approved application specification.
Discuss Your Component
To discuss precision threaded rod, send Romy the controlled drawing, mating requirements, intended material condition and expected order quantities. Identify socket contact as the point requiring review, and request a written feasibility response with any process exceptions before tooling or production is released.
See the M12 Ball Head Upper Pressure Rod product example and contact Romy with the drawing revision for your project.
Frequently Asked Questions
What should be defined first for precision threaded rod?
Identify the surfaces that establish position and the mating parts that constrain them. That determines which dimensions and relationships require specific control.
Can a matching nominal size prove compatibility?
No. Profile, engagement depth, corner geometry and final surface condition can change fit even when a principal size matches.
Should every tolerance be made tighter?
No. Tighten requirements where the assembly needs them and verify the manufacturing and inspection consequences before releasing the revision.
What makes a fit trial repeatable?
Use identified mating components, a controlled assembly condition and a record of entry, seating and final position.
What should the supplier return for precision threaded rod?
A drawing-based feasibility review, identified exceptions, proposed process route and a plan for verifying the functional features.